
Hydraulic System Maintenance for Concrete Mixing Pumps: Common Mistakes
Hydraulic System Maintenance for Concrete Mixing Pumps
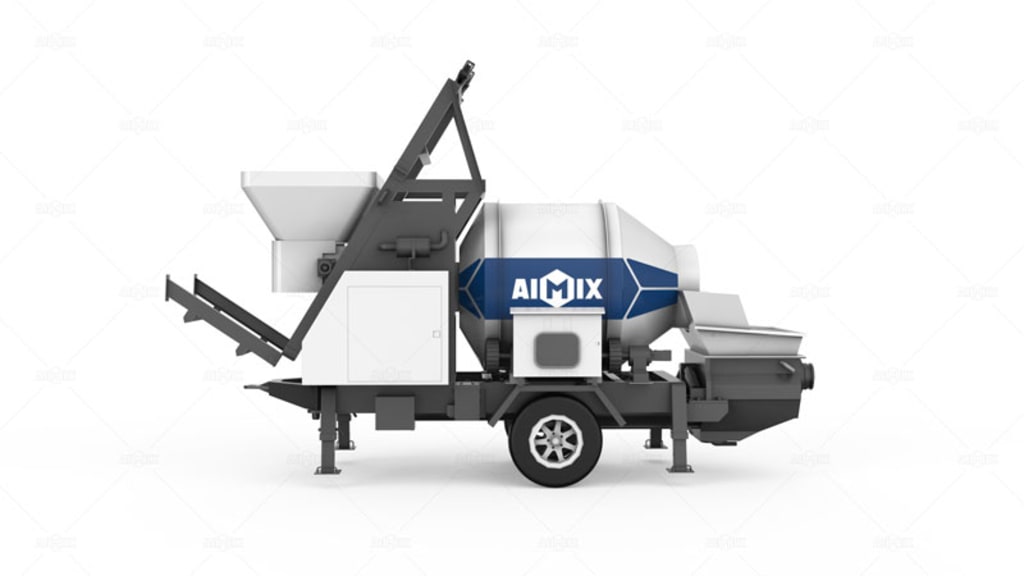
Welcome to the beating heart of your concrete mixing pump—the hydraulic system! This pressurized network of pumps, valves, and actuators is what gives your equipment its formidable strength and smooth, metered delivery. Yet, it's astonishing how often this critical system is treated as an afterthought. Operators frequently fall into predictable traps, turning minor oversights into catastrophic, wallet-draining failures. Understanding these common mistakes isn't just about avoiding breakdowns; it's about unlocking the longevity and peak performance your machine was built to deliver. Let's dive headfirst into these pitfalls and chart a course toward proactive, enthusiastic care!
Mistake One: The Peril of Improper Fluid Selection and Contamination
The lifeblood of any hydraulic system is its fluid, yet choosing it often becomes a game of guesswork. Reaching for any "hydraulic oil" on the shelf is a recipe for disaster. Concrete pumps operate under punishing, variable loads and extreme temperatures. Using a fluid with the wrong viscosity index can starve the pump at startup or fail to lubricate when the system sizzles. Worse, many ignore the specter of contamination. Microscopic particles from concrete dust, water ingress, or degraded seals act like sandpaper inside精密 tolerances. This isn't mere speculation; it's a mechanical certainty.
Subheading: The Viscosity Villain and the Additive Arsenal
Check your manufacturer's specifications obsessively. A fluid too thick on a cold morning leads to cavitation—the silent destroyer of pump internals. Conversely, a thin, overheated fluid loses its film strength, allowing metal-on-metal galling. Beyond viscosity, modern fluids boast additive packages: anti-wear (AW), rust inhibitors, and foam suppressants. Do not assume these are standard. Verify them. When topping off, use the exact same brand and formulation. Mixing different additive chemistries can create a gel-like sludge, a nightmare to flush. Treat your fluid reservoir with the reverence of a chemical laboratory.
Subheading: Filtration Fallacies and the Sampling Imperative
A common cry is, "I changed the filter last month!" But are you changing the right filter, at the right interval, and inspecting the old one? A collapsed filter element indicates excessive pressure drop, often from a cold start on thick oil. A filter filled with brass or steel glitter means active component wear. Do not merely swap elements; perform regular oil sampling. Send a vial of your hydraulic fluid for a particle count analysis. This spectrographic examination reveals contamination levels invisible to the naked eye. Establish a baseline, then track trends. An upward spike in silicon (dust) or water content is your early warning system.
Mistake Two: Neglecting the Thermal Regime and Overheating
Heat is the arch-nemesis of hydraulic efficiency. Every component, from the piston pump to the directional valve, is designed to operate within a specific thermal window, typically 100-140°F (38-60°C). Exceed this, and seals harden, fluid oxidizes into varnish, and clearances tighten until something seizes. Operators often ignore rising temperatures, thinking, "It's just a hot day." This is a dangerous rationalization. An overheating system is screaming for attention. The culprits are often deceptively simple: a clogged cooler core, a faulty bypass valve on the return filter, or continuous operation at the pressure relief valve's set point.
Subheading: Cooler Conundrums and Idle-Time Idioms
Inspect your oil cooler religiously. Concrete dust and airborne debris act as a perfect insulating blanket. A pressure washer or compressed air directed through the fins can work wonders. But do not stop there. Verify the cooler's fan engages at the correct setpoint. Listen for unusual sounds from the fan motor—grinding bearings reduce airflow dramatically. Furthermore, educate operators on the virtues of idle time. Running the portable concrete pump against a closed valve or holding a concrete line under pressure without flow generates immense, wasted heat. Implement a rule: if you aren't placing concrete for more than two minutes, relieve the pressure and let the oil circulate freely.
Subheading: The Varnish Verdict and Fluid Replacement Rhythm
When hydraulic oil repeatedly overheats, it undergoes pyrolysis, leaving behind a sticky, amber-hued varnish on internal surfaces. This varnish adheres to valve spools, causing them to stick or move sluggishly. It insulates heat exchangers, worsening the problem. The solution is not just a fluid change, but a system flush using specialized detergents. Establish a rigorous fluid replacement schedule based on hours and analysis, not calendar months. A pump working a single eight-hour shift accumulates degradation differently than one operating around the clock. Be methodical, not arbitrary.
Mistake Three: Ignoring the Tell-Tale Signs of Wear and Loose Connections
Hydraulic systems communicate their health through subtle cues. A pump that once growled quietly now emits a distinct whine. A cylinder cycle time increases by a fraction of a second. A fitting develops a microscopic weep, not a full leak. These are the whispers of impending component failure. The common mistake is to dismiss them as "normal wear" until the whisper becomes a shout—a burst hose, a seized pump, or a concrete line that suddenly has no pressure. Proactive observation is your cheapest and most effective maintenance tool.
Subheading: Decoding the Language of Leaks and Loose Fasteners
Do not tolerate any leakage, regardless of how minor. A few drops per minute from a threaded fitting might seem inconsequential, but it admits air. Air in a hydraulic system causes spongy, erratic actuator control and catastrophic pump damage through micro-dieseling. Use a torque wrench on every JIC or ORFS fitting during reassembly. Over-tightening is as destructive as under-tightening, distorting seats and creating stress risers. Periodically check the bolts securing the pump to its mounting flange and the motor to its bracket. Vibration is relentless; it will loosen these fasteners, leading to misalignment and premature shaft or coupling failure.
Subheading: Cylinder Syncopation and Hose Armor
For pumps with twin-cylinder concrete delivery, monitor the synchronization. If one cylinder consistently finishes its stroke before the other, a bypassing piston seal or a malfunctioning cartridge valve is the suspect. This asynchronous behavior drastically reduces volumetric efficiency and places asymmetric loads on the rock valve. Simultaneously, inspect every hydraulic hose. Look for blistering, chafing against frames, or a stiff, "crackled" feel to the rubber cover. These hoses are under immense cyclic pressure. A catastrophic rupture sprays hot oil—a fire hazard and an environmental nightmare. Replace hoses on a schedule, not after they fail.
About the Creator
AIMIX
Construction Machine Manufacturer in China. Find Machines here: https://aimixconcretesolution.com/
Enjoyed the story? Support the Creator.
Subscribe for free to receive all their stories in your feed.
Comments